Product Overview
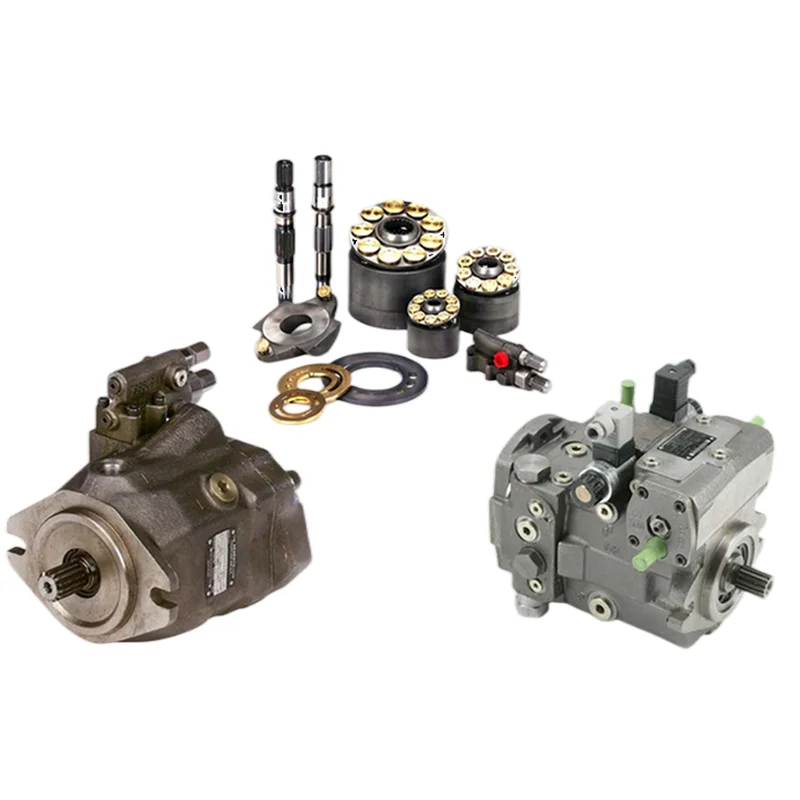
The A2FE Series hydraulic pump repair kit is a high-quality replacement parts set specifically designed for Bosch Rexroth A2FE bent-axis axial piston fixed displacement pumps/motors, covering the full range of A2FE 23, 28, 32, 45, 56, 63, 80, 90, 107, 125, 160, 180, 200, 250, 355, 500, and 1000 displacement sizes. The A2FE series features a bent-axis design with axial tapered piston rotary group, suitable for hydrostatic drives in open and closed circuits, and is widely deployed in concrete mixer drum drives, road roller wheel drives, excavator auxiliary drives, mining machinery, and heavy-duty construction equipment.
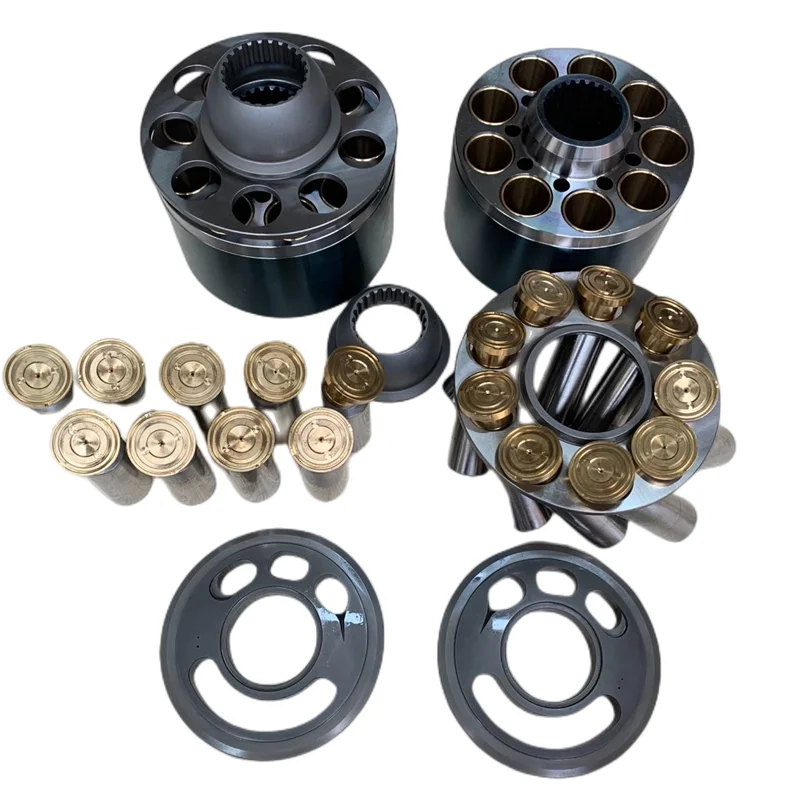
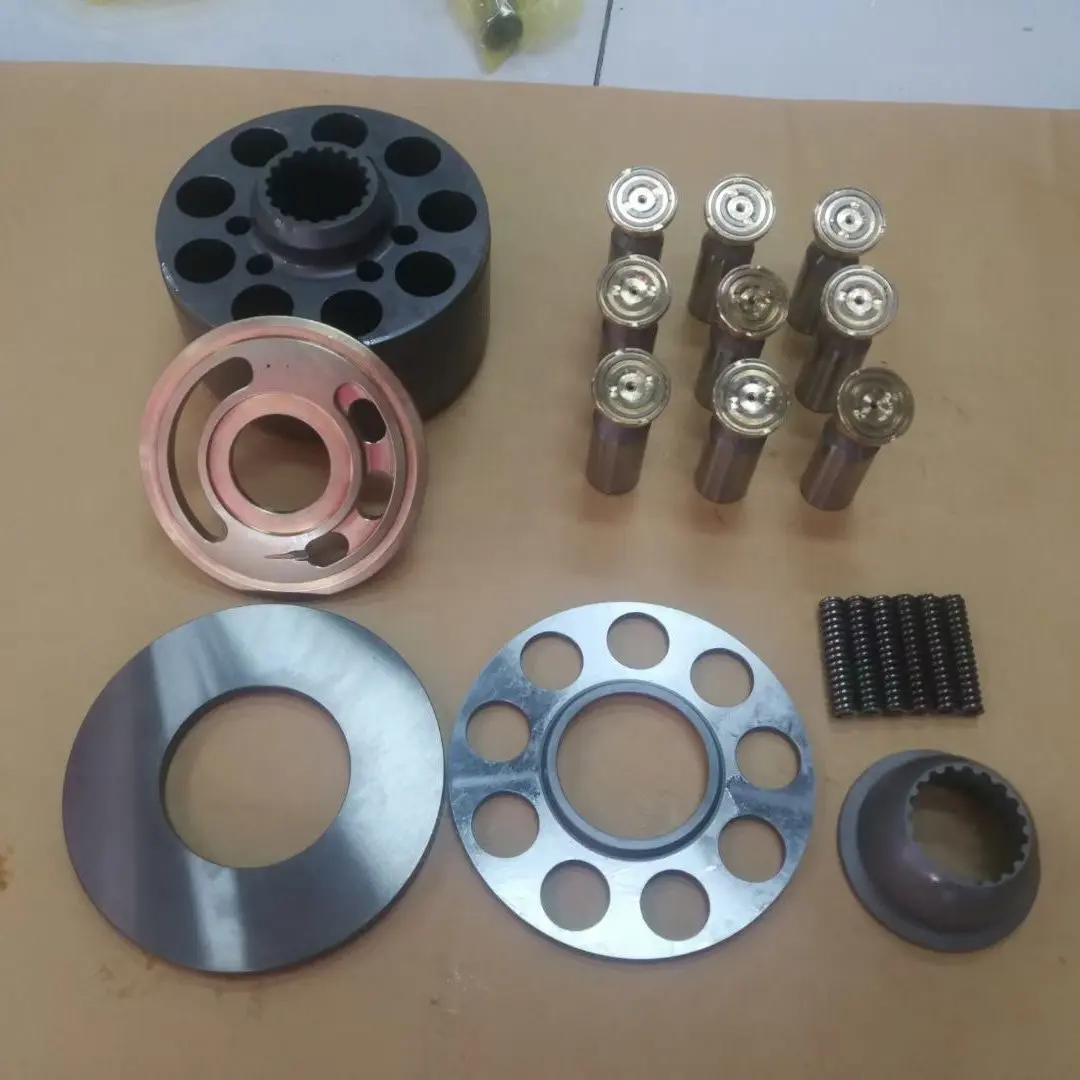
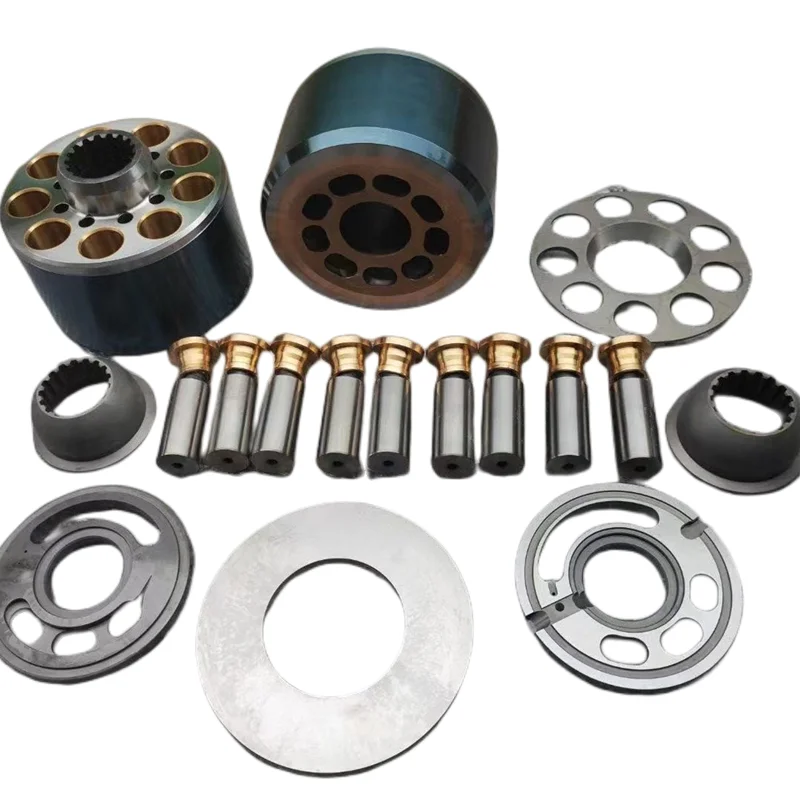
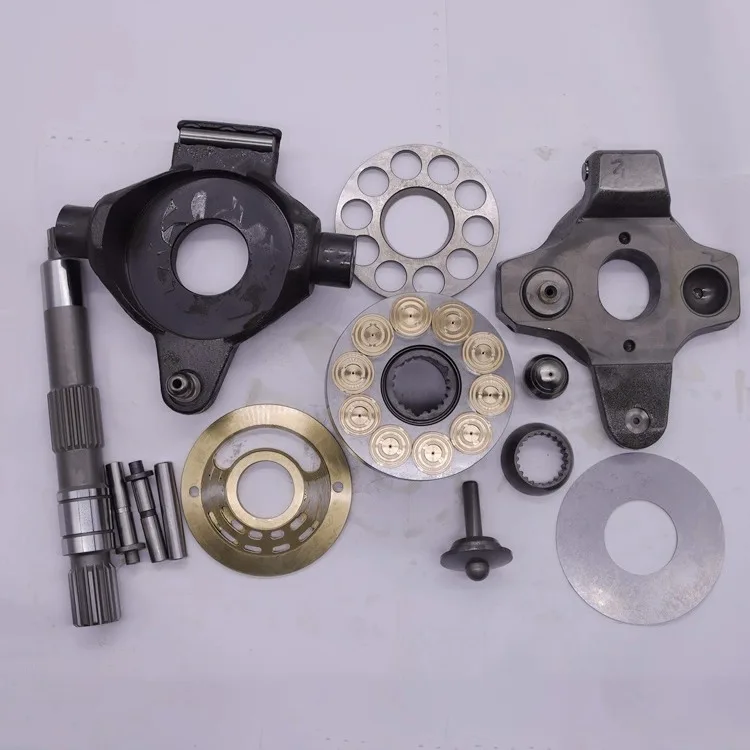
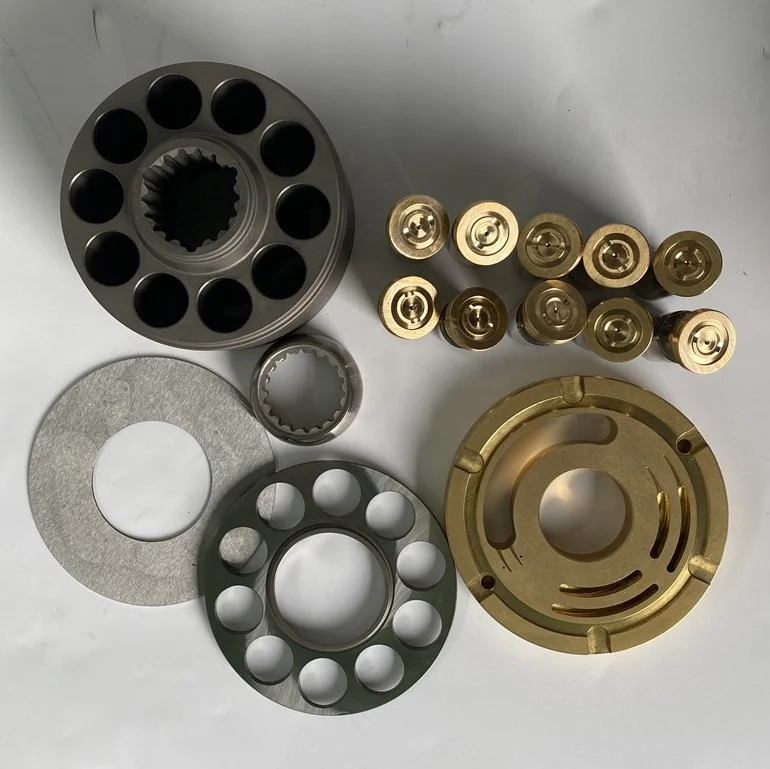
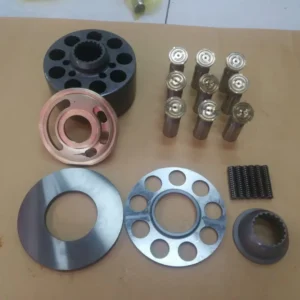
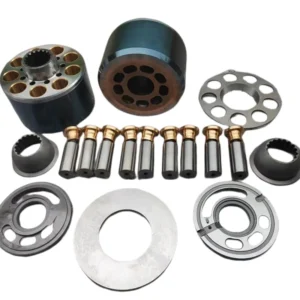
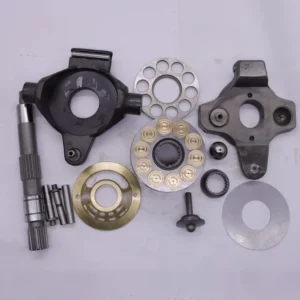
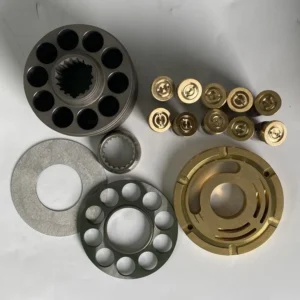
The repair kit includes cylinder block, valve plate, piston with ring, retainer plate (set plate), ball guide, center pin, drive shaft, cradle bearing seat, saddle bearing, and a complete seal kit. All components are manufactured strictly to Rexroth OEM technical standards, with cylinder block and valve plate manufactured using matched lapping processes and pistons precision-matched to cylinder bores, ensuring 100% drop-in interchangeability without requiring installation interface modifications or additional machining.
The A2FE series employs a bent-axis design in which the spherical porting between cylinder block and valve plate enables automatic self-centering during rotation, resulting in low peripheral speed and high volumetric efficiency. The drive shaft is supported by heavy-duty rolling bearings capable of withstanding radial loads, suitable for belt-drive or gear-drive installation. Engineering specifications require that cylinder block and valve plate be replaced as a matched pair, and pistons be replaced as a complete set, which is the critical requirement for ensuring volumetric efficiency and smooth operation after repair.
Every A2FE Series repair kit undergoes 100% dimensional inspection and material verification prior to shipment, with critical fit dimensions cross-referenced against original drawings to ensure restored A2FE pumps/motors return to OEM performance levels.
Technical Specifications
A2FE Series Core Product Parameters (Complete Pump/Motor Technical Data):
Product Series: Bosch Rexroth A2FE Series 6x/7x
Pump/Motor Type: Bent-axis axial piston fixed displacement pump/motor
Design Type: Bent-axis axial tapered piston rotary group, fixed displacement, plug-in/standard flange mounting
Circuit Compatibility: Open circuit and closed circuit hydrostatic drives
Displacement Coverage: 23.1, 28.1, 32, 45.6, 56.1, 63, 80.4, 90, 106.7, 125, 160.4, 180, 200, 250, 355, 500, 1000 cm³/rev
Nominal Pressure: 400 bar (40 MPa), for sizes 28–180
Maximum Pressure: 450 bar (45 MPa), for sizes 28–180
Nominal Pressure (200–355 sizes): 350 bar (35 MPa)
Maximum Pressure (200–355 sizes): 400 bar (40 MPa)
Maximum Speed Range: 2650–4750 rpm (depending on displacement size)
Drive Shaft Load Capability: Can withstand radial loads, suitable for belt/gear drives
Mounting Type: Plug-in or standard SAE flange
Fluid Compatibility: Mineral-based hydraulic oil, fire-resistant hydraulic oil
Operating Temperature Range: 30–90 ℃
A2FE Series Individual Displacement Technical Data:
A2FE23: 23.1 cm³/rev, rated 3750 rpm, max 6300 rpm
A2FE28: 28.1 cm³/rev, rated 2240 rpm, max 4750 rpm, weight 10.5 kg
A2FE32: 32.0 cm³/rev, rated 2240 rpm, max 4750 rpm, weight 10.5 kg
A2FE45: 45.6 cm³/rev, rated 2000 rpm, max 4250 rpm, weight 15 kg
A2FE56: 56.1 cm³/rev, rated 1800 rpm, max 3750 rpm, weight 18 kg
A2FE63: 63.0 cm³/rev, rated 1800 rpm, max 3750 rpm, weight 19 kg
A2FE80: 80.4 cm³/rev, rated 1600 rpm, max 3350 rpm, weight 23 kg
A2FE90: 90.0 cm³/rev, rated 1600 rpm, max 3350 rpm, weight 25 kg
A2FE107: 106.7 cm³/rev, rated 1400 rpm, max 3000 rpm, weight 34 kg
A2FE125: 125.0 cm³/rev, rated 1400 rpm, max 3000 rpm, weight 36 kg
A2FE160: 160.4 cm³/rev, rated 1250 rpm, max 2650 rpm, weight 47 kg
A2FE180: 180.0 cm³/rev, rated 1250 rpm, max 2650 rpm, weight 48 kg
A2FE200: 200 cm³/rev, nominal 350 bar, peak 400 bar
A2FE250: 250 cm³/rev, nominal 350 bar, peak 400 bar
A2FE355: 355 cm³/rev, nominal 350 bar, peak 400 bar
Repair Kit Component List:
Cylinder Block / Barrel: Precision matched lapping, spherical porting surface
Valve Plate / Control Plate: Matched lapping with cylinder block, paired replacement
Piston with Ring / Piston Assembly: Complete set replacement, precision-fitted to cylinder bores
Retainer Plate / Set Plate: Piston retraction retention
Ball Guide: Rotary group guidance
Center Pin: Cylinder positioning and drive
Drive Shaft: Heavy-duty alloy steel, radial load capability
Cradle Bearing Seat: Swashplate support
Saddle Bearing: Swashplate kinematic pair
Complete Seal Kit: NBR/FKM material, including shaft seal, O-rings, back-up rings
Key Technical Advantages
1. Bent-Axis Design — High Volumetric Efficiency and Self-Centering
The A2FE series employs a bent-axis design with axial tapered piston rotary group, in which spherical porting between the cylinder block and valve plate enables automatic self-centering during rotation, resulting in low peripheral speed and high volumetric efficiency. The spherical porting design maintains excellent port plate contact under high pressure, reducing internal leakage. The cylinder block and valve plate in this repair kit are manufactured strictly to OEM spherical matched lapping specifications, ensuring the restored pump/motor recovers its original high volumetric efficiency level. The drive shaft is supported by heavy-duty rolling bearings capable of withstanding radial loads, suitable for belt-drive or gear-drive installation.
2. Precision Matched Lapping Process — Paired Cylinder Block and Valve Plate Replacement
The interface between cylinder block and valve plate in A2FE pumps/motors is the most critical friction pair in the rotary group, with its flatness and surface finish directly determining volumetric efficiency and internal leakage levels. The cylinder block and valve plate in this repair kit are manufactured using matched lapping processes, ensuring the fit clearance between them meets OEM specifications. Engineering specifications require that cylinder block and valve plate be replaced as a matched pair, and pistons be replaced as a complete set — the critical requirement for ensuring smooth operation and consistent service life after repair.
3. Heavy-Duty Drive Shaft and Bearing System — Heavy-Duty Reliability
The drive shaft of A2FE series pumps/motors is manufactured from high-strength alloy steel, supported by heavy-duty ball bearings and roller bearings capable of withstanding significant radial loads, suitable for plug-in applications directly mounting drive wheels or gears. The drive shaft, cradle bearing seat, and saddle bearing in this repair kit are manufactured to OEM material and heat treatment specifications, ensuring long-term reliable operation under heavy-duty conditions. This design makes A2FE pumps/motors particularly suitable for road roller wheel drives, concrete mixer drum drives, and other heavy-duty applications.
4. Complete Seal Kit — Restores Factory Sealing Performance
This repair kit includes a complete seal kit covering shaft seals, O-rings, back-up rings, and all sealing elements. Seals are manufactured from NBR or FKM material, suitable for mineral-based hydraulic oil and fire-resistant hydraulic oil. Seal dimensions and materials match OEM specifications, ensuring leak-free operation of the restored pump/motor within rated pressure and temperature ranges. During installation, pay attention to the orientation of the shaft seal lip, ensuring the sealing lip faces the pressure side.
5. 100% Drop-in Interchangeability — Direct Replacement Without Machining
All components in this repair kit are manufactured to Rexroth A2FE Series OEM technical drawings, with critical fit dimensions and tolerances corresponding one-to-one with original components. The cylinder block, valve plate, piston set, drive shaft, and other core components can be installed directly into original A2FE pump/motor housings without additional machining or adaptation modifications. The repair kit covers the full A2FE 23–1000 displacement range, with repair kits for different displacement sizes within the same series supplied independently in corresponding dimensions for precise matching.
Application Areas
Concrete Mixer Trucks: Mixing drum drive motor (A2FE107/125/160/180) repair, restoring drum drive torque output
Road Rollers: Travel drive motor (A2FE45/56/63/80) repair, restoring travel drive performance
Excavators: Auxiliary drive motor (A2FE107/125/160) repair for swing or travel auxiliary drives
Mining Machinery: Heavy-duty mining equipment hydraulic motor repair, for A2FE125/160/180/200/250/355 sizes
Drilling Equipment: Drill rig swing and travel drive motor repair
Construction Machinery: Crawler crane and rotary drilling rig hydraulic motor repair
Industrial Hydraulics: Fixed hydraulic power units and test bench A2FE motor repair
This repair kit is suitable for major overhaul and refurbishment of A2FE series pumps/motors across all displacement sizes, particularly suitable for equipment users requiring restored factory performance while controlling repair costs.
Expert Maintenance Tips
1. Pre-Repair Fault Diagnosis and Confirmation
Before ordering a repair kit, systematic fault diagnosis should be performed on the A2FE pump/motor to confirm the failure mode. Common failure causes include: cylinder block and valve plate wear caused by hydraulic oil contamination, increased clearance between pistons and cylinder bores, shaft runout caused by bearing wear, and seal aging and shaft seal leakage. It is recommended to record operating parameters (pressure, flow, temperature, noise) before disassembly, and measure rotary group components after disassembly to confirm the specific component replacement scope.
2. Disassembly and Cleaning Specifications
Disassembling the A2FE pump/motor should be performed in a clean environment, using specialized tools to avoid damaging mating surfaces. After disassembly, all parts should be cleaned with clean hydraulic oil or specialized cleaning agents; never use cotton waste or materials that may shed fibers to wipe precision mating surfaces. After cleaning, blow dry with compressed air (avoid directing high-speed airflow directly at bearings). The mating surfaces of cylinder block, valve plate, and piston set should be inspected with a magnifying glass to confirm no scratches, scoring, or abnormal wear marks.
3. Critical Control Points During Assembly
During assembly, all mating surfaces should be coated with clean hydraulic oil; never assemble dry. Piston sets must be replaced as a complete set; never mix new and old pistons, to ensure consistent clearance between all pistons and cylinder bores. Cylinder block and valve plate must be replaced as a matched pair; ensure correct positioning of the valve plate locating pin during assembly. When installing the drive shaft, check bearing clearance; spline or keyed shaft engagement with the coupling should ensure sufficient engagement length. All bolts should be tightened in diagonal sequence to specified torque; apply grease to the seal lip when installing the shaft seal.
4. Post-Repair Commissioning and Performance Verification
The repaired A2FE pump/motor should be commissioned before being placed into service. Before initial startup, prime the housing through the case drain port with clean hydraulic oil. Commissioning should be performed at low speed and low pressure for 10–15 minutes, checking case drain flow, shaft seal leakage, operating noise, and vibration. Gradually load to rated pressure and speed, monitoring volumetric efficiency recovery. During commissioning, closely monitor oil temperature changes and system pressure stability.
5. Hydraulic System Cleaning and Contamination Control
The service life of A2FE rotary group components — particularly the interface between cylinder block and valve plate — is strictly dependent on hydraulic fluid cleanliness. When installing the repair kit, the hydraulic system must be thoroughly cleaned, all filter elements replaced, and the reservoir and piping flushed. Recommended fluid cleanliness is ISO 18/16/13 (NAS Class 8) or better, using 10 μm pressure line filters. When the old pump/motor failed due to mechanical failure, metal particles may remain in the system and must be completely removed through flushing circuits before installing the repaired pump/motor.